Stable oil-in-water emulsions can resist the gravity separation expected for free oil. Chemical demulsification should therefore be selected through representative trials and linked to the equipment that removes the destabilized material. Industrial buyers need to evaluate clarified water, recovered oil and sludge together when comparing complete treatment offers.
Distinguish stable emulsion from free oil
A stable oil-in-water emulsion contains dispersed droplets whose coalescence is inhibited by the mixture’s chemistry and physical condition. It may not separate adequately in equipment selected for free oil. Identify the production fluids, detergents and surfactants reaching the wastewater before proposing chemical treatment. The objective of demulsification is to destabilize the dispersion so an appropriate subsequent step can remove the separated material. It does not by itself prove that the remaining dissolved organic load is acceptable for biological treatment, reuse or discharge.
Translate this distinction into a purchase boundary for industrial oily wastewater chemical demulsification. List the equipment that delivers the stated function and the upstream conditions supplied by the owner. Ask bidders to explain exclusions in the same schedule as included items. A technically complete offer should identify what remains uncertain and which additional observation would resolve it. Keep those open items visible when comparing prices, because a smaller scope can otherwise appear to offer the same duty.
Collect samples that represent the production mixture
Include relevant machining fluids, wash solutions, batch dumps and cleaning changes in the sampling plan. Record dilution, temperature, storage time and any upstream chemical additions. A convenient surface sample can overrepresent free oil while missing the stable emulsion entering treatment. Keep the original source description with each trial sample. Ask whether collection or transport has already changed the emulsion before interpreting a favorable result. Different production formulations may require separate test cases even when they are all reported under the same oil-and-grease heading.
Use the production schedule to choose the sampling campaign for industrial oily wastewater chemical demulsification. Include normal manufacture, cleaning transitions and relevant changes of raw material. Label historical measurements with their dates and methods. If a difficult condition has never been measured, identify it as a design assumption rather than averaging it into an apparently precise specification. Agree how a later change in the feed envelope will be reviewed before extending an equipment guarantee to that new condition.
Send the feed-water analysis, target quality, required capacity and operating profile. We will help structure the next engineering questions.
Send your project inputsUse jar trials to select a controlled sequence
Compare suitable chemical routes through an approved laboratory protocol that records addition order, mixing, pH, temperature and separation time. Do not choose an acid or coagulant solely from another factory’s recipe. Evaluate the whole treated-water and residuals result rather than visual clarity alone. Where a trial uses heating or substantial pH adjustment, include the required utility or neutralization duty in the proposed scope. Retain the least favorable credible feed result so selection is not based only on the most easily broken sample.
Place the proposed arrangement on the actual site drawing before releasing the order. Trace every inlet, outlet and utility from an identified source to an identified destination. Include space for isolation and maintenance, with ownership of each connection written beside the package boundary. The drawing review for industrial oily wastewater chemical demulsification should resolve conflicts while changes are still straightforward, rather than leaving the installation contractor to interpret several separate vendor drawings during commissioning.
Match the destabilized material to its separator
The conditioned mixture still requires removal of oil-rich material, floc or another separated phase. Connect the chemical trial to the intended flotation, gravity or other suitable separation step. Review pumps and transfer mixing that could alter the material between conditioning and removal. Identify whether the trial predicts floating, settling or mixed residual behaviour and how the installed separator will accommodate it. A successful jar test cannot establish full-scale removal if the layout destroys the separation structure or gives it insufficient time to develop.
Write a cause-and-effect schedule that operators can use during a shift. Distinguish a valid result, a held value and a failed measurement. Identify who may change settings and what evidence permits a return to service. Demonstrate the important states using approved simulations where direct fault creation would be inappropriate. A control display for industrial oily wastewater chemical demulsification should preserve the reason for a stop instead of clearing all evidence as soon as the operator presses reset.
Evaluate water quality and residual destinations together
Measure the attributes relevant to the downstream process, such as oil-and-grease, solids, organic loading and chemical compatibility, using agreed methods. Some dissolved constituents may remain even after visible oil separation. Characterize recovered oil and sludge before assigning a disposal or recovery route. Added treatment chemicals can change residual quantity and handling. Include sludge dewatering and return-water consequences where they affect plant capacity. Do not describe the separated oil as a saleable recovered product without evidence of its actual quality and an identified receiving route.
Request a maintenance demonstration using the delivered configuration. The team should be able to identify the exact replacement part, reach it with the intended tools and verify the restored condition. Record the observations that trigger inspection and keep the manufacturer's operating restrictions with the work instruction. For industrial oily wastewater chemical demulsification, spare availability and access can be as important to continuity as the nominal equipment rating, particularly when the plant has limited staffed maintenance windows.
Accept a repeatable trial-to-plant operating window
Document the feed envelope, selected chemistry, dosing sequence and mixing arrangement used for acceptance. Test the response to a changed source, failed dosing or ineffective separation with appropriate approved procedures. Keep field observations tied to samples and operating events so operators can recognize when the agreed recipe no longer applies. A clear effluent sample from one production batch is insufficient evidence for all future coolant or detergent formulations. Final handover should state when a new jar trial is required and who approves changes to the chemical programme.
Convert acceptance into a witnessed record with agreed instruments, sample locations and operating conditions. Separate functional checks from process results and state which deviations require another trial. Retain raw observations alongside calculated conclusions so later troubleshooting can reproduce the decision. The handover for industrial oily wastewater chemical demulsification should include configuration revisions and unresolved restrictions, allowing a new engineer to understand the proven operating boundary without relying on recollections from the original commissioning team.
Build the quotation and handover around a measured duty
Prepare the enquiry for industrial oily wastewater chemical demulsification with the available analysis, operating schedule, utility conditions and a marked layout. State whether Baihuipu is reviewing a new package, an equipment replacement or integration into an existing treatment train. Ask the proposal to address emulsion stability, chemical trial sequence and downstream separation and to identify any specialist supply or additional testing needed. Compare the same included scope across bids, including commissioning, recurring supplies and the owner responsibilities needed to support the proposed duty. Technical exceptions should have an accountable owner and a planned resolution before the supply agreement is finalized.
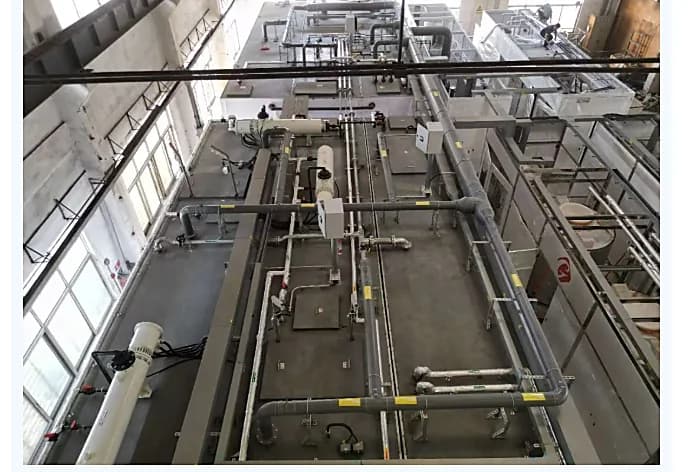
Retain the selected design basis with the operating manual and review it when production changes. A revised cleaning chemical, different wastewater source or altered shift pattern can invalidate assumptions that were reasonable at purchase. Site-specific evidence should determine the next engineering action; this guide supplies a framework for that review and makes no universal performance or cost-saving promise. The featured photograph provides actual industrial water-treatment equipment context. It does not establish that the specialist component described here appears in the image, or demonstrate a customer result, certification or completed project.
Questions buyers commonly ask
Will a free-oil coalescer always remove a stable emulsion?+
No. Stable dispersions can require destabilization or a different treatment route. Identify the emulsion and trial the actual wastewater before selecting the complete separation system.
Is clear water from a jar test sufficient acceptance?+
No. Measure relevant downstream water attributes and characterize residuals. Visual clarity does not establish removal of dissolved organics or compatibility with reuse and biological treatment.
When should the chemical recipe be reviewed?+
Review it when production fluids, detergents, feed proportions or separation behaviour change. Preserve the trial record and use representative new testing before extending the original operating window.
Turn the guide into a project brief.
Final process selection and performance commitments should follow the complete feed-water analysis, application requirements, site utilities and approved technical agreement.